Contents
Counterfeit prevention starts before incoming inspection. Strong controls generally combine approved sourcing channels, supplier qualification, manufacturer or distributor documentation, lot and date-code records, packaging review, incoming inspection, controlled storage and proportionate testing for higher-risk parts.
Electronic component traceability preserves the relationship among the purchased component, supplier, manufacturer, lot or date code, receiving record and production batch where the project requires it. No single document or inspection method proves authenticity in every case, so controls should increase with sourcing risk.
| Control | Purpose | Limitation |
|---|---|---|
| Authorized sourcing | Reduce provenance risk | Availability may be limited |
| Supplier qualification | Control the sourcing process | Requires ongoing review |
| COC/documentation | Preserve traceability | Documents alone do not prove authenticity |
| Packaging/label inspection | Detect inconsistencies | Sophisticated counterfeits may pass |
| Visual inspection | Identify obvious anomalies | Has limited diagnostic power |
| Electrical testing | Verify defined device behavior | Coverage depends on the test plan |
| X-ray/advanced analysis | Inspect internal structure | Is not required for every part |
| Lot/date-code records | Connect material to the build | Depend on disciplined recordkeeping |
What is electronic component traceability?
Electronic component traceability is the documented chain connecting a manufacturer identity and part number to the supplier, purchase record, received lot, inspection record and production use. The required depth depends on customer, application and quality-system requirements.
Traceability does not always mean serializing every component or finished unit. For many builds, lot-level association is appropriate; other programs may require tighter unit or batch controls. Define the requirement before purchasing so records are captured rather than reconstructed later.
What is a counterfeit electronic component?
A counterfeit component is intentionally misrepresented as to its identity, source, condition, grade or performance. Conceptual examples include remarked devices, recycled parts sold as new, altered lot or date codes, cloned devices, misrepresented temperature or speed grades, and tampered packaging.
A nonconforming or damaged genuine part is not automatically counterfeit. Separating authenticity, quality and handling failures helps the team select the right containment and investigation path.
Authorized and independent supply channels
Authorized distribution provides a manufacturer-recognized commercial chain and usually stronger access to manufacturer documentation and support. Independent distributors and brokers can provide legitimate material when authorized stock is unavailable, but provenance may be less direct.
No channel removes every possible quality risk. Risk controls should become stronger as the chain of custody becomes less direct, especially for obsolete, scarce, high-value or safety-relevant parts. Independent supply should be evaluated, not condemned categorically.
Supplier qualification
Supplier qualification is the process of deciding whether a source can meet defined commercial, quality and traceability requirements. Review sourcing policy, documented quality history, provenance records, return and nonconformance handling, responsiveness and the ability to provide required documentation.
An approved supplier list should be maintained and periodically reviewed under the customer’s or manufacturer’s quality system. Approval is not permanent proof for every transaction; purchase-specific risks still need assessment.
Verify the complete manufacturer part number
The complete manufacturer part number identifies more than a device family. Suffixes can specify package, speed, temperature grade, memory, tolerance, lead finish, RoHS status or packing form.
Compare the BOM, purchase order, manufacturer data and received label. A partial MPN can produce a perfectly genuine but technically wrong component. Resolve ambiguity before placing the order rather than relying on a description after receipt.
Packaging and label inspection
Inspect whether reels, trays, tubes, moisture-barrier bags, seals and labels are consistent with the ordered part and documented source. Compare manufacturer identity, full MPN, quantity, lot and date codes, packaging form and any moisture or handling information.
Inconsistent printing, seals or records can justify escalation, but a packaging checklist is not definitive proof of authenticity. Sophisticated counterfeit material may imitate labels, while legitimate repacking may create explainable differences. Preserve evidence and ask the supplier to reconcile discrepancies.
Visual component inspection
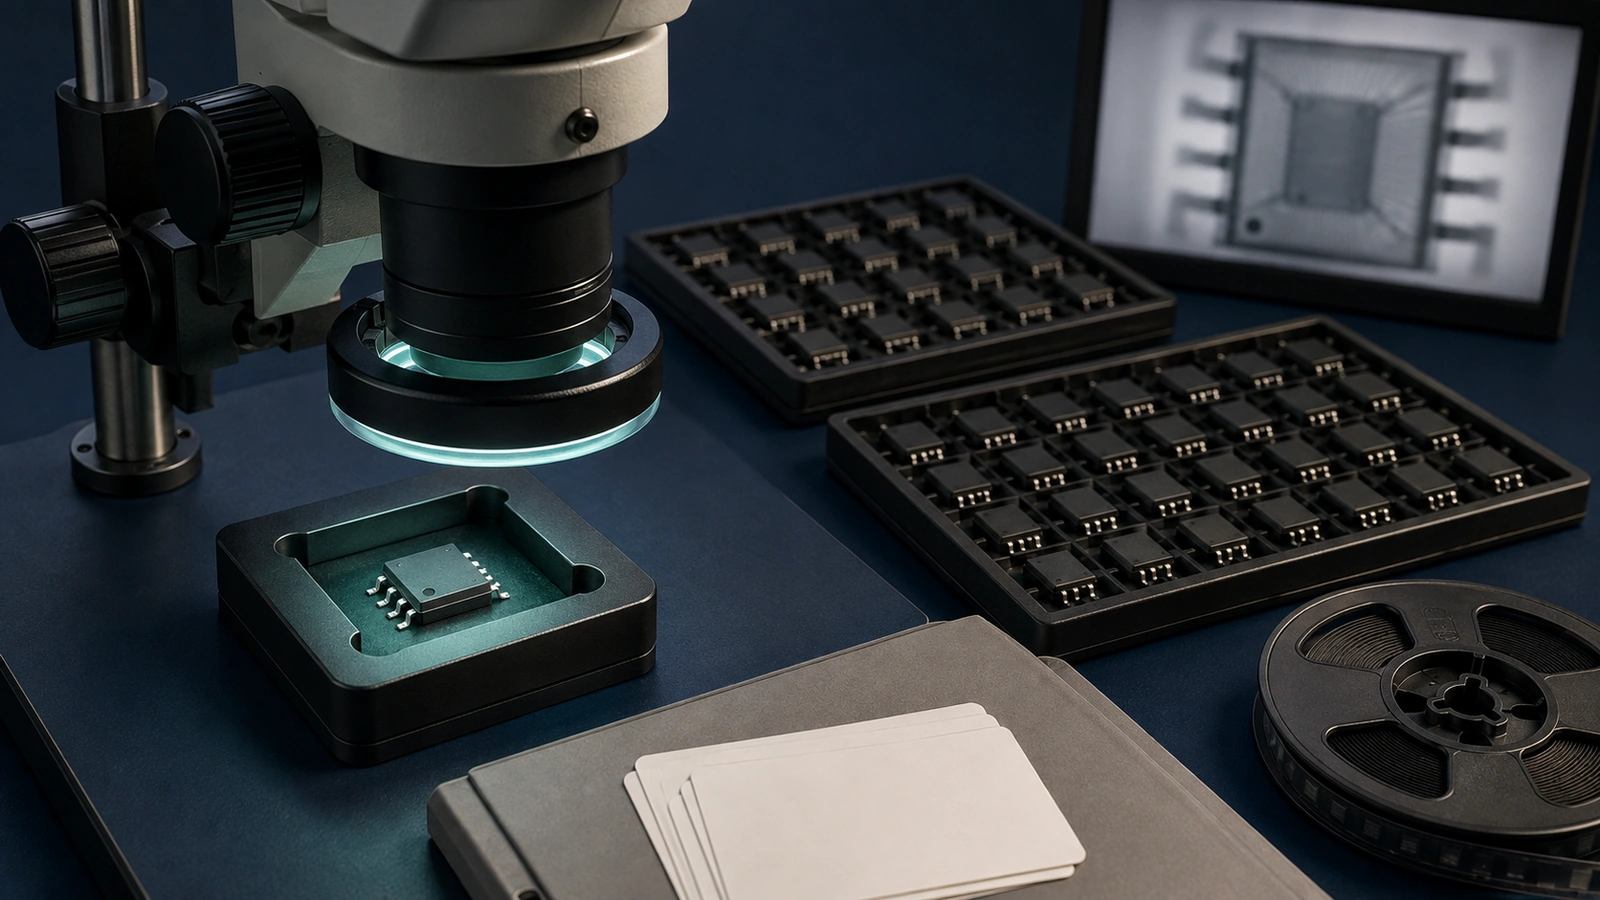
Visual inspection can identify inconsistent markings, resurfacing indicators, damaged or oxidized leads, contamination, package damage, and unusual mold or finish variation. Use suitable magnification, lighting, sampling and reference information for the risk level.
Visual inspection has limited diagnostic power. Manufacturing variations, multiple assembly sites and legitimate lots can differ. An anomaly is a reason for controlled review, not an automatic counterfeit verdict.
Electrical testing
Electrical testing checks whether samples meet defined functional or parametric requirements. The plan can range from basic identification and electrical checks to application-specific functional validation, using current manufacturer limits where appropriate.
Test coverage depends on the device, equipment, sample plan and accessible functions. Passing a limited test does not fully authenticate a complex device, and destructive or exhaustive testing is not practical for every lot. Match the method to the consequence and evidence gap.
X-ray and advanced inspection
X-ray can compare internal construction, die position, bond-wire patterns and other structural features without opening the package. X-ray fluorescence may help characterize material composition, while decapsulation and other specialist analyses can provide deeper evidence.
These methods require appropriate references and expertise. X-ray alone does not prove authenticity, and destructive physical analysis is not automatically justified. Escalate higher-risk or unresolved material to a qualified testing resource with a documented question and sampling plan.
Moisture sensitivity, storage and handling
Authenticity and quality are separate issues. A genuine component can be damaged by moisture exposure, oxidation, electrostatic discharge, poor storage or handling. Incoming controls should therefore address packaging condition, moisture controls where applicable, ESD handling and storage environment.
Detailed moisture-sensitivity levels, floor life and bake decisions deserve their own manufacturing review. Here, the essential control is to preserve the supplied handling status and record any deviation before assembly.
Date codes and lot codes
Date and lot codes support traceability by connecting components to a manufacturing group or time period under the manufacturer’s coding system. They help investigate failures, mixed lots and affected production builds.
A different date code is not automatically counterfeit. Multiple legitimate lots can be supplied, and coding formats vary. Confirm the customer’s mixing restrictions, record what was received and assess unexplained inconsistencies together with source, packaging and test evidence.
Traceability during PCB assembly
Assembly traceability associates incoming component lots with the receiving record, work order or build lot, inspection results and nonconformance records. The system should identify where controlled material was used and what disposition applied to rejected or suspect material.
Complete unit-level component genealogy should not be claimed unless the process and customer requirement support it. Define the association level, retention period and documents before the build. First article inspection can verify assembly and documentation against the approved production baseline, but it does not replace source control.
High-risk sourcing scenarios
Risk commonly increases when a part is obsolete, a severe shortage removes authorized stock, pricing is unusually low for the documented market, supply combines unexplained mixed lots, or excess inventory lacks provenance. These conditions are indicators, not proof of counterfeit material.
Use the obsolete-component sourcing guide when availability drives the problem. If a different part is proposed, route it through alternate-component engineering review rather than treating authenticity testing as a substitute for compatibility.
Risk-based counterfeit prevention workflow
- Verify the complete manufacturer part number and required grade.
- Check lifecycle and the available source path.
- Select a sourcing channel appropriate to the risk.
- Verify supplier approval and transaction-specific capability.
- Obtain required purchase and provenance documentation.
- Inspect packaging, seals, labels and received quantity.
- Perform incoming inspection under the defined sampling plan.
- Escalate higher-risk or inconsistent material for suitable testing.
- Preserve lot, receiving, storage and production records.
- Segregate and control nonconforming or suspect material.
A BOM risk analysis can identify which line items deserve stronger sourcing controls before purchase.
Electronic component traceability checklist
A practical receiving record should identify the purchase order, supplier, full MPN, manufacturer, quantity, packaging form, received lot/date codes, receipt date and inspection disposition. Attach the documentation required by the purchase agreement, and record any discrepancy rather than overwriting the original label information. A certificate of conformity is supporting evidence from its issuer; its value depends on the issuer, scope and connection to the actual material.
For example, two reels carrying different legitimate date codes may be acceptable for a commercial build with no lot-mixing restriction. The receiving team should still preserve both codes and associate the reels with the build. The same delivery may require escalation for a customer that explicitly requires one manufacturing lot. The difference is the agreed requirement and traceability evidence, not an assumption that mixed dates prove counterfeiting.
When a discrepancy remains unresolved, quarantine the affected material and prevent it from entering the production kit. Record the quantity, physical location, reason for hold and responsible reviewer. Keep the supplier’s response and any test evidence with the disposition. Do not blend suspect material into accepted stock, relabel it to conceal the discrepancy or use a passing functional sample to erase an unresolved provenance question.
The escalation question should be specific: does the material match the ordered grade, can the supplier explain the chain of custody, are markings consistent with an authoritative reference, or does an electrical parameter meet its specified limit? A clear question helps a testing resource propose relevant methods. A generic request to “prove the parts are genuine” can encourage an expensive test package without defining what uncertainty remains after testing.
Manufacturer policies are also relevant to support and warranty expectations. Texas Instruments’ anti-counterfeit guidance identifies its authorized purchasing routes and warns about provenance risks outside them. Review the policy for the actual manufacturer rather than assuming all manufacturers support or authenticate independently sourced material in the same way. This is a sourcing decision input, not a claim that every independent distributor supplies counterfeit parts.
Before release, reconcile the material record with the work order and any customer documentation package. If the process tracks components only to a build lot, describe that level accurately. A traceability claim should never be broader than the records that production can retrieve during an investigation.
- Supplier: approval status, source role and quality contact are recorded.
- Manufacturer: identity and complete MPN match the requirement.
- Purchase order: grade, packaging, documentation and restrictions are stated.
- Lot/date code: received codes and any mixing constraints are recorded.
- Packaging: reel, tray, tube, labels, seals and moisture protection are reviewed.
- Inspection: method, sample, evidence, result and inspector are retained.
- Storage: ESD, moisture and environmental controls are maintained.
- Production lot: material is associated at the required work-order, batch or unit level.
- Nonconformance: segregation, investigation, disposition and supplier response are controlled.
- Customer records: certificates and traceability package meet the agreed requirement.
Information required from the customer
Provide the BOM with full manufacturer part numbers, approved supplier or manufacturer lists, approved alternates, traceability requirements and restricted sourcing channels. Also identify production quantity, customer or industry quality requirements, certificate expectations and record-retention needs.
Excel Circuit’s component sourcing service can coordinate BOM review, documented sourcing and production material controls within a turnkey PCBA workflow.
Plan traceability before purchasing begins
Send your BOM and sourcing requirements if you need component availability, traceability and sourcing-risk review before PCBA production. State the required documentation and any prohibited channels so the controls can be built into the purchase plan.